Alu Alu Cold Blister Films Market Outlook
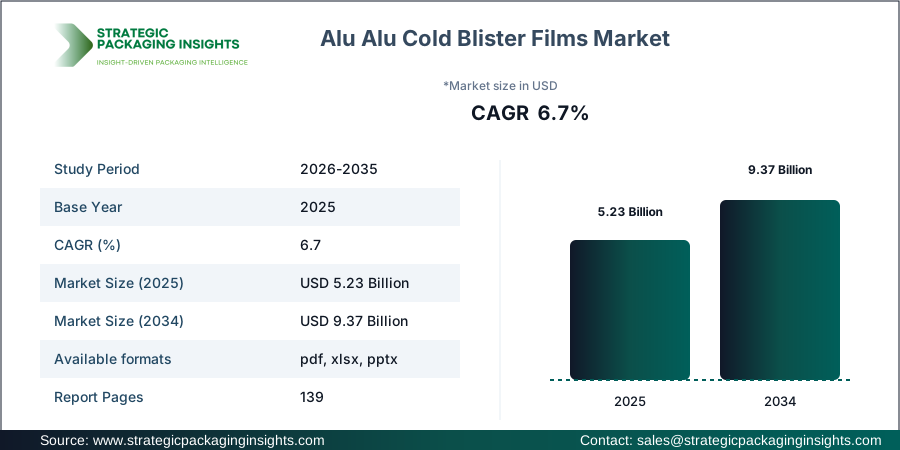
The Alu Alu Cold Blister Films market size was valued at USD $5.23 Bn in 2025 and is anticipated to reach USD $9.37 Bn by 2035, growing at a CAGR of 6.7% % during the forecast period according to Strategic Packaging Insights. The increasing demand for high-barrier packaging solutions in the pharmaceutical industry is a significant driver, as these films provide superior protection against moisture, oxygen, and light, ensuring the stability and efficacy of sensitive formulations.Report Scope
| Attributes | Details |
| Report Title | Alu Alu Cold Blister Films Market Projected to Scale to 9.37 Billion by 2035, Assesses Strategic Packaging Insights |
| By Material Type | Aluminum Foil, Polyamide, PVC, Laminated Films |
| By Application | Tablets, Capsules, High-Barrier Drugs, Sensitive Formulations |
| By End Use | Pharmaceutical Companies, CDMOs, Nutraceutical Brands |
| By Barrier Type | Moisture Barrier, Oxygen Barrier, Light Barrier |
| Region | Asia Pacific, North America, Latin America, Europe, Middle East & Africa |
| Base Year | 2025 |
| Historic Period | 2018-2024 |
| Forecast Period | 2026-2035 |
| Number of Pages | 139 |
| Customization Available | Yes* |
Market Trends Analysis
Alu Alu Cold Blister Films are witnessing increased adoption due to their superior barrier properties, which are crucial for protecting sensitive pharmaceutical formulations. The trend towards personalized medicine and the rise in chronic diseases are driving demand for specialized packaging solutions. Additionally, the shift towards sustainable packaging is influencing manufacturers to explore recyclable and eco-friendly materials, impacting product development and procurement strategies.
Technological advancements in film manufacturing, such as improved lamination and coating techniques, are enhancing the performance of Alu Alu Cold Blister Films. The integration of digital printing technologies is enabling customization and improving supply chain efficiency. These trends are reshaping competitive dynamics, encouraging investments in R&D, and fostering collaborations between pharmaceutical companies and packaging suppliers.
Industry Transformation Analysis
The Alu Alu Cold Blister Films industry is undergoing significant transformation driven by advancements in manufacturing technologies and a shift towards sustainable practices. The adoption of automation and digitalization in production processes is enhancing operational efficiency and reducing costs. This transformation is leading to increased capacity and improved product quality, enabling companies to meet the growing demand for high-barrier packaging solutions.
Value-chain transformation is evident as companies focus on vertical integration to secure raw material supply and enhance control over production processes. The emphasis on sustainability is prompting investments in recycling technologies and the development of eco-friendly materials. These changes are influencing procurement strategies, with companies prioritizing suppliers that align with their sustainability goals and regulatory requirements.
Trends & Disruptions Impacting Customers' Customers
Pharmaceutical companies, the primary end-users of Alu Alu Cold Blister Films, are increasingly focusing on product differentiation and patient-centric packaging solutions. The demand for high-barrier films is driven by the need to protect sensitive formulations and extend product shelf life. Regulatory requirements for packaging safety and efficacy are also influencing purchasing decisions, with companies seeking suppliers that can meet stringent standards.
These downstream changes are impacting the Alu Alu Cold Blister Films market by driving innovation and encouraging the development of advanced materials with enhanced barrier properties. Suppliers are investing in R&D to offer customized solutions that meet the specific needs of pharmaceutical companies. This trend is creating opportunities for market growth and fostering collaborations between packaging manufacturers and pharmaceutical firms.
Alu Alu Cold Blister Films Market Ecosystem
The Alu Alu Cold Blister Films market ecosystem involves a complex value chain from raw material procurement to recycling. The procurement of high-quality aluminum foil, polyamide, and PVC is critical for producing films with superior barrier properties. Film production involves advanced lamination and coating techniques to ensure product efficacy and safety.
Converting processes transform these films into blister packs, which are then distributed to pharmaceutical companies and contract development and manufacturing organizations (CDMOs). The distribution stage is crucial for maintaining supply chain efficiency and meeting demand. Recycling and end-of-life processing are becoming increasingly important as sustainability becomes a priority, influencing procurement strategies and material flows.
Analyst Perspective
Analyst Perspective: The Alu Alu Cold Blister Films market is poised for significant growth driven by the pharmaceutical industry's demand for high-barrier packaging solutions.
The most important structural change is the shift towards sustainable packaging, which is influencing material selection and driving innovation in film manufacturing. Companies are focusing on developing recyclable and eco-friendly materials to meet regulatory requirements and consumer expectations.
Market participants should monitor advancements in film manufacturing technologies and sustainability initiatives. These factors are critical for maintaining competitive advantage and meeting the evolving needs of pharmaceutical companies. Strategic collaborations and investments in R&D will be key to capturing market opportunities and driving growth.
Opportunities & Threats
The Alu Alu Cold Blister Films market presents significant opportunities driven by the increasing demand for high-barrier packaging solutions in the pharmaceutical industry. The rise in chronic diseases and the trend towards personalized medicine are creating a need for specialized packaging that ensures product stability and efficacy. Companies that can offer innovative and customized solutions are well-positioned to capture market share.
Technological advancements in film manufacturing, such as improved lamination and coating techniques, are enhancing product performance and creating opportunities for differentiation. The integration of digital printing technologies is enabling customization and improving supply chain efficiency, further driving market growth.
However, the market faces threats from raw material price volatility and regulatory uncertainty. The reliance on aluminum foil and other materials can lead to cost fluctuations, impacting profitability. Additionally, stringent regulatory requirements for packaging safety and efficacy pose challenges for manufacturers, requiring continuous investment in compliance and quality assurance.
Competition from alternative packaging solutions and the need for sustainable practices are also significant threats. Companies must navigate these challenges by investing in R&D and developing eco-friendly materials to meet consumer and regulatory demands. Strategic partnerships and collaborations will be essential for overcoming these threats and maintaining market position.
Drivers & Challenges
The primary driver of the Alu Alu Cold Blister Films market is the pharmaceutical industry's demand for high-barrier packaging solutions. These films provide superior protection against moisture, oxygen, and light, ensuring the stability and efficacy of sensitive formulations. The rise in chronic diseases and the trend towards personalized medicine are further driving demand for specialized packaging solutions.
Regulatory requirements for packaging safety and efficacy are also influencing market growth. Companies are investing in advanced materials and technologies to meet stringent standards and ensure compliance. The emphasis on sustainability is prompting the development of recyclable and eco-friendly materials, aligning with consumer and regulatory expectations.
Challenges in the market include raw material price volatility and regulatory uncertainty. The reliance on aluminum foil and other materials can lead to cost fluctuations, impacting profitability. Additionally, stringent regulatory requirements pose challenges for manufacturers, requiring continuous investment in compliance and quality assurance. Companies must navigate these challenges by investing in R&D and developing innovative solutions to maintain market position.
Packaging Market Economics
The economics of Alu Alu Cold Blister Films are influenced by raw material costs, including aluminum foil, polyamide, and PVC. These materials are critical for producing films with superior barrier properties, impacting procurement strategies and pricing. Conversion costs, including lamination and coating processes, are significant factors in determining product pricing and profitability.
Energy costs and logistics also play a crucial role in the overall economics of Alu Alu Cold Blister Films. Efficient supply chain management and distribution are essential for maintaining competitive pricing and meeting demand. Companies are investing in advanced manufacturing technologies to enhance operational efficiency and reduce costs, ensuring sustainable growth in the market.
Packaging Value Chain & Cost Analysis
The value chain for Alu Alu Cold Blister Films involves multiple tiers, from resin synthesis and substrate production to converting and distribution. Tier-3 includes resin synthesis and the production of aluminum foil, polyamide, and PVC. Tier-2 involves film extrusion and substrate production, where raw materials are transformed into films with superior barrier properties.
Tier-1 encompasses converting, printing, and lamination processes, where films are transformed into blister packs for pharmaceutical applications. Downstream activities include co-packing, distribution, and recycling, ensuring efficient supply chain management and end-of-life processing. Companies are focusing on optimizing each tier to enhance operational efficiency and reduce costs, ensuring sustainable growth in the market.
Unit Economics & Substrate Cost Analysis
The unit economics of Alu Alu Cold Blister Films are influenced by raw material costs, including aluminum foil, polyamide, and PVC. These materials are critical for producing films with superior barrier properties, impacting procurement strategies and pricing. Conversion costs, including lamination and coating processes, are significant factors in determining product pricing and profitability.
Energy costs and logistics also play a crucial role in the overall economics of Alu Alu Cold Blister Films. Efficient supply chain management and distribution are essential for maintaining competitive pricing and meeting demand. Companies are investing in advanced manufacturing technologies to enhance operational efficiency and reduce costs, ensuring sustainable growth in the market.
Packaging Regulatory & Sustainability Analysis
The Alu Alu Cold Blister Films market is subject to stringent regulatory requirements for packaging safety and efficacy. Regulatory bodies such as the FDA and EMA set standards for packaging materials used in pharmaceutical applications, influencing material selection and product development. Companies must ensure compliance with these regulations to maintain market access and avoid penalties.
Sustainability is a key focus, with increasing emphasis on developing recyclable and eco-friendly materials. Regulatory initiatives such as the European Commission's Circular Economy Action Plan are driving the adoption of sustainable practices in packaging. Companies are investing in R&D to develop materials that meet regulatory requirements and align with consumer expectations for sustainability.
Strategic Mergers, Acquisitions & Capacity Expansions
Recent strategic developments in the Alu Alu Cold Blister Films market include mergers, acquisitions, and capacity expansions by key players. Companies are focusing on expanding their production capabilities and enhancing their product portfolios to meet growing demand. Strategic partnerships and collaborations are also being pursued to leverage technological advancements and enhance market presence.
For instance, Amcor has invested in expanding its production facilities to increase capacity and meet the rising demand for high-barrier packaging solutions. Similarly, Constantia Flexibles has focused on strategic acquisitions to enhance its product offerings and strengthen its market position. These developments are expected to drive market growth and create opportunities for innovation and differentiation.
Strategic Action Directives
Brand Packaging Engineers & Sustainability Directors should focus on material selection and mono-material qualification to enhance barrier performance and recyclability. Integrating PCR into packaging solutions can align with sustainability goals and regulatory requirements.
Converter Operations & Extrusion Leads should optimize line speed, tooling, and changeover processes to enhance operational efficiency and reduce scrap. Managing PCR variability and capacity utilization is crucial for maintaining competitive advantage.
Procurement & Material Sourcing Managers should focus on securing resin contracts and price indexing to mitigate raw material price volatility. Diversifying suppliers and managing EPR exposure can enhance supply chain resilience.
Investors should monitor capacity expansions, margin structures, and M&A activities to identify growth opportunities. Understanding market concentration and technology advancements can inform strategic investment decisions.
Market Share Analysis
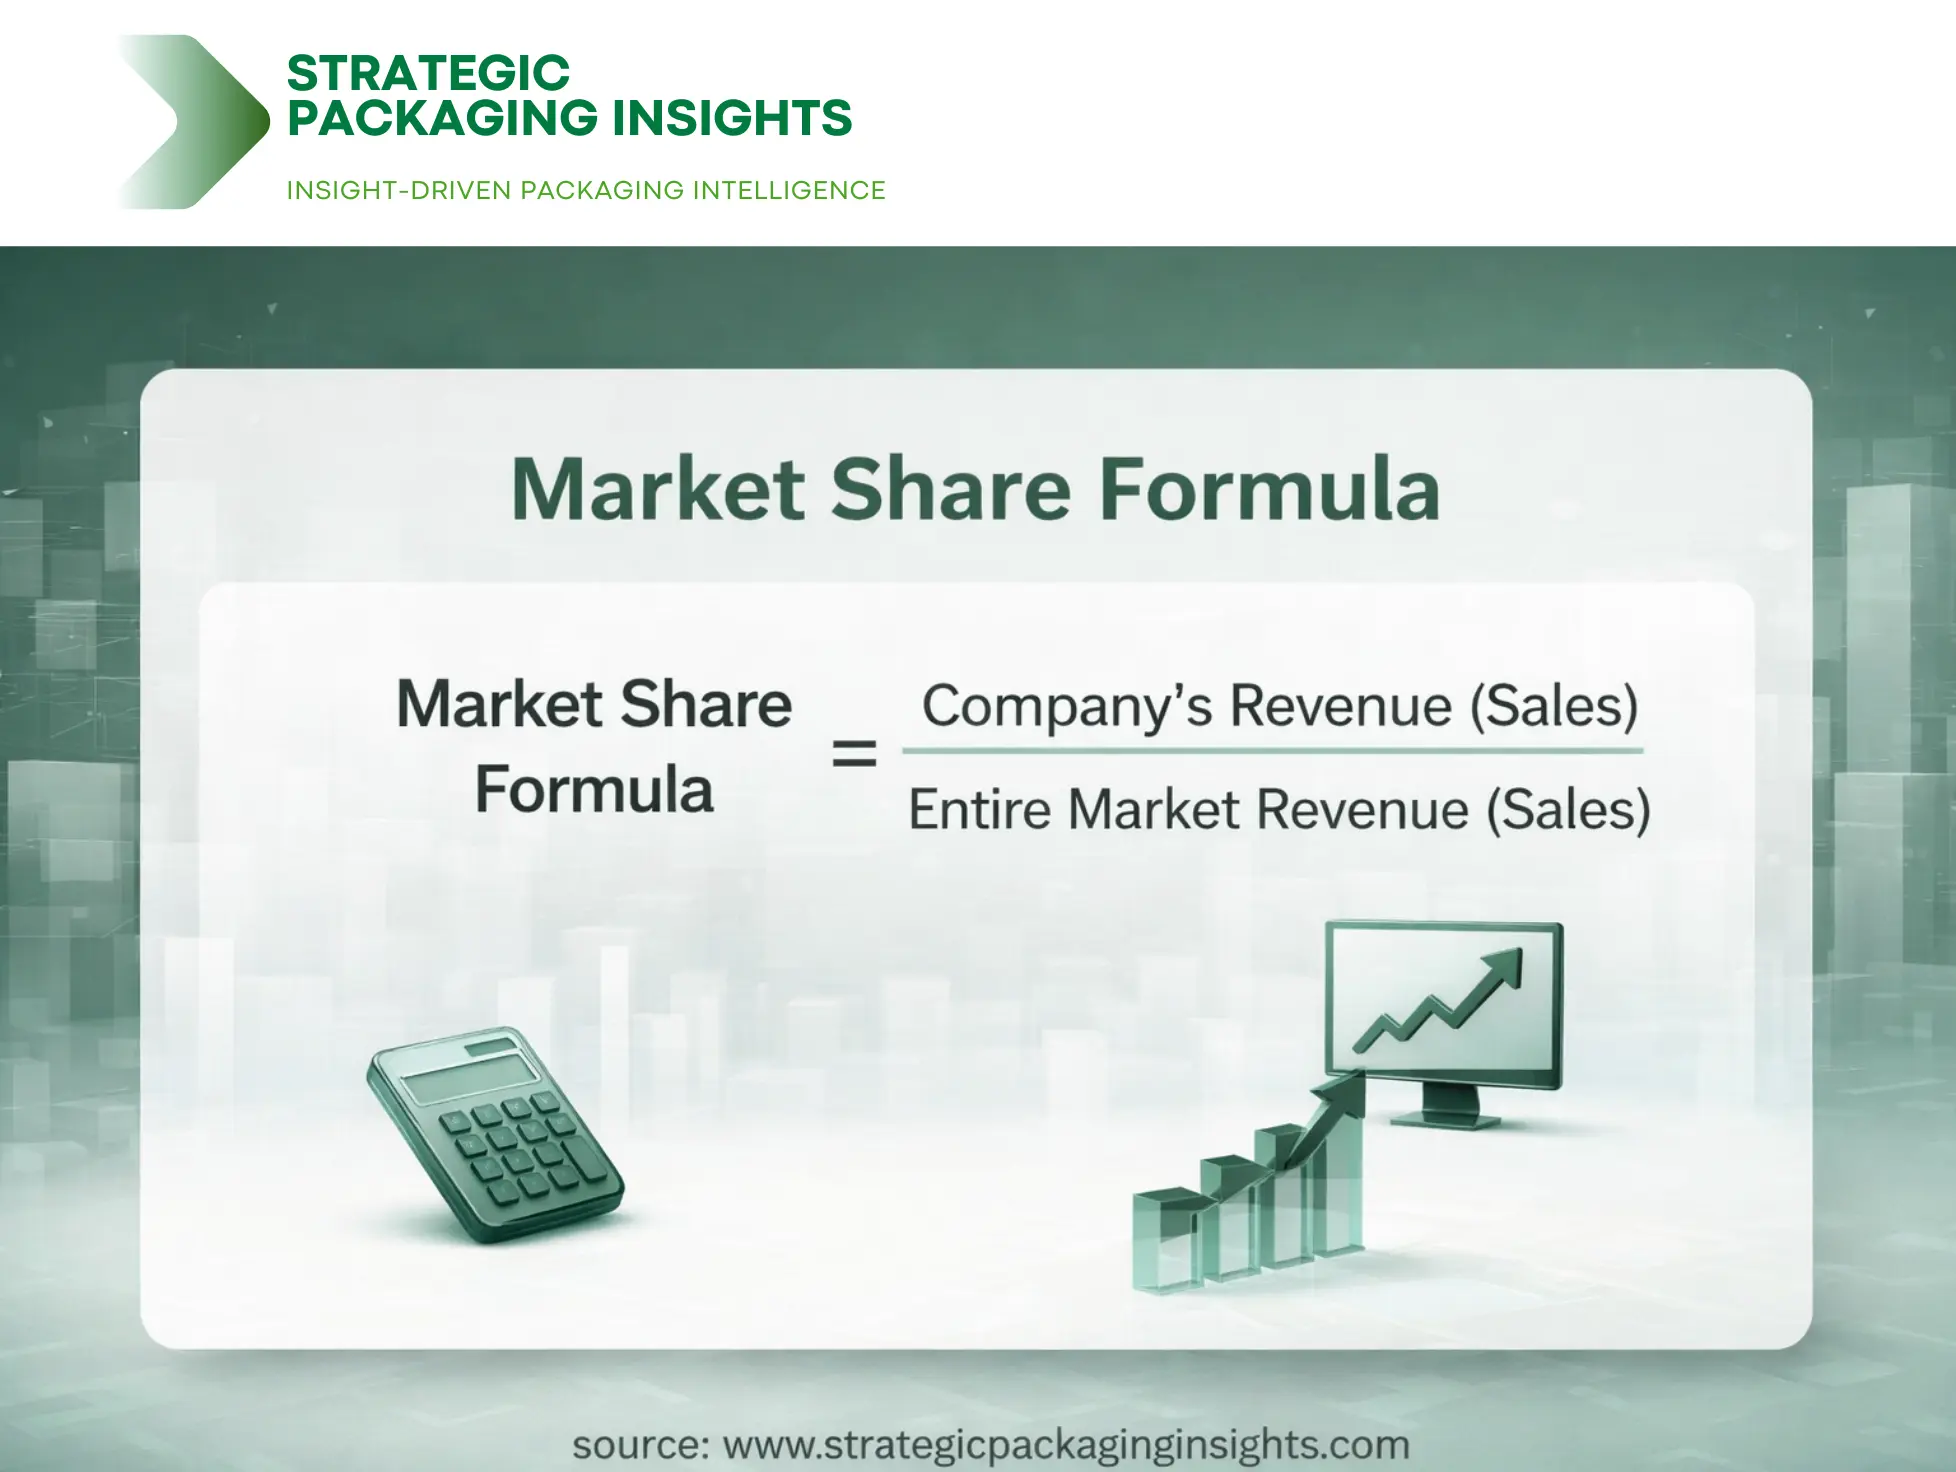
The Alu Alu Cold Blister Films market is characterized by a competitive landscape with several key players holding significant market shares. Companies such as Amcor, Constantia Flexibles, and UFlex are leading the market with their extensive product portfolios and strong geographic presence. These companies are focusing on innovation and sustainability to maintain their competitive edge.
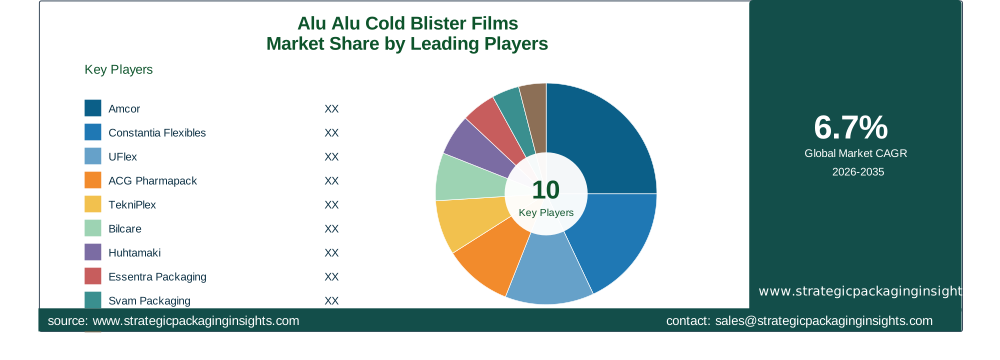
Amcor is a prominent player in the market, offering a wide range of high-barrier packaging solutions. The company's focus on sustainability and innovation has strengthened its market position. Constantia Flexibles is another key player, known for its advanced film manufacturing technologies and commitment to sustainability.
UFlex is a leading manufacturer of Alu Alu Cold Blister Films, with a strong presence in Asia Pacific and a focus on expanding its global footprint. The company's investments in R&D and capacity expansions have enhanced its competitive position. ACG Pharmapack and TekniPlex are also significant players, offering innovative packaging solutions and focusing on strategic partnerships to drive growth.
Other notable companies in the market include Bilcare, Huhtamaki, Essentra Packaging, Svam Packaging, and Wipak. These companies are investing in advanced manufacturing technologies and sustainability initiatives to enhance their market presence and meet the evolving needs of pharmaceutical companies.
Key Highlights
- Largest Region: Asia Pacific
- Fastest-Growing Region: Asia Pacific
- Largest Segment: Pharmaceutical Companies
- Fastest-Growing Segment: High-Barrier Drugs
- Base-year market size: $5.23 Bn
- Forecast-year market size: $9.37 Bn
- CAGR: 6.7%
- Important application: Tablets
- Major end-use industry: Pharmaceutical Companies
- Major market driver: Demand for high-barrier packaging solutions
Regional Insights
The Alu Alu Cold Blister Films market is witnessing significant growth across major regions, with Asia Pacific emerging as the largest and fastest-growing region. The demand for high-barrier packaging solutions in the pharmaceutical industry is driving market growth, particularly in emerging economies.
North America
North America is a mature market for Alu Alu Cold Blister Films, with a strong focus on innovation and sustainability. The presence of major pharmaceutical companies and stringent regulatory requirements are driving demand for high-barrier packaging solutions. The region is characterized by advanced manufacturing technologies and a focus on sustainability initiatives.
The demand for Alu Alu Cold Blister Films in North America is driven by the need for specialized packaging solutions that ensure product stability and efficacy. The emphasis on sustainability is influencing material selection and driving innovation in film manufacturing.
Europe
Europe is a significant market for Alu Alu Cold Blister Films, with a strong focus on sustainability and regulatory compliance. The region is characterized by stringent packaging regulations and a commitment to sustainable practices. The demand for high-barrier packaging solutions is driven by the need to protect sensitive pharmaceutical formulations.
The emphasis on sustainability is influencing material selection and driving innovation in film manufacturing. Companies are investing in advanced technologies to enhance product performance and meet regulatory requirements.
Asia Pacific
Asia Pacific is the largest and fastest-growing region for Alu Alu Cold Blister Films, driven by the increasing demand for high-barrier packaging solutions in the pharmaceutical industry. The region is characterized by rapid industrialization and a growing focus on healthcare infrastructure.
The demand for Alu Alu Cold Blister Films in Asia Pacific is driven by the need for specialized packaging solutions that ensure product stability and efficacy. The emphasis on sustainability is influencing material selection and driving innovation in film manufacturing.
Latin America
Latin America is an emerging market for Alu Alu Cold Blister Films, with a growing focus on healthcare infrastructure and pharmaceutical manufacturing. The demand for high-barrier packaging solutions is driven by the need to protect sensitive formulations and extend product shelf life.
The emphasis on sustainability is influencing material selection and driving innovation in film manufacturing. Companies are investing in advanced technologies to enhance product performance and meet regulatory requirements.
Middle East & Africa
The Middle East & Africa region is witnessing growing demand for Alu Alu Cold Blister Films, driven by the increasing focus on healthcare infrastructure and pharmaceutical manufacturing. The demand for high-barrier packaging solutions is driven by the need to protect sensitive formulations and extend product shelf life.
The emphasis on sustainability is influencing material selection and driving innovation in film manufacturing. Companies are investing in advanced technologies to enhance product performance and meet regulatory requirements.
Alu Alu Cold Blister Films Market Segments Insights

By Material Type Analysis
The Alu Alu Cold Blister Films market is segmented by material type, including aluminum foil, polyamide, PVC, and laminated films. Aluminum foil is the most widely used material due to its superior barrier properties, providing protection against moisture, oxygen, and light. Polyamide and PVC are also popular choices, offering flexibility and durability.
The demand for laminated films is driven by the need for enhanced barrier performance and customization options. Companies are investing in advanced manufacturing technologies to develop innovative materials that meet the evolving needs of pharmaceutical companies. The emphasis on sustainability is influencing material selection, with a focus on developing recyclable and eco-friendly options.
By Application Analysis
The Alu Alu Cold Blister Films market is segmented by application, including tablets, capsules, high-barrier drugs, and sensitive formulations. Tablets and capsules are the most common applications, driven by the need for specialized packaging solutions that ensure product stability and efficacy.
The demand for high-barrier drugs and sensitive formulations is increasing due to the rise in chronic diseases and the trend towards personalized medicine. Companies are investing in advanced materials and technologies to develop packaging solutions that meet the specific needs of these applications. The emphasis on sustainability is influencing product development, with a focus on developing recyclable and eco-friendly options.
By End Use Analysis
The Alu Alu Cold Blister Films market is segmented by end use, including pharmaceutical companies, CDMOs, and nutraceutical brands. Pharmaceutical companies are the largest end-use segment, driven by the need for high-barrier packaging solutions that ensure product stability and efficacy.
CDMOs and nutraceutical brands are also significant end-users, with a focus on developing specialized packaging solutions that meet the specific needs of their products. The emphasis on sustainability is influencing material selection and driving innovation in film manufacturing. Companies are investing in advanced technologies to enhance product performance and meet regulatory requirements.
By Barrier Type Analysis
The Alu Alu Cold Blister Films market is segmented by barrier type, including moisture barrier, oxygen barrier, and light barrier. Moisture barrier films are the most widely used, providing protection against moisture and ensuring product stability and efficacy.

Oxygen barrier films are also popular, offering protection against oxygen and extending product shelf life. Light barrier films are used to protect sensitive formulations from light exposure, ensuring product stability and efficacy. Companies are investing in advanced materials and technologies to develop innovative barrier solutions that meet the evolving needs of pharmaceutical companies.
Alu Alu Cold Blister Films Market Segments
The Alu Alu Cold Blister Films market has been segmented on the basis ofBy Material Type
- Aluminum Foil
- Polyamide
- PVC
- Laminated Films
By Application
- Tablets
- Capsules
- High-Barrier Drugs
- Sensitive Formulations
By End Use
- Pharmaceutical Companies
- CDMOs
- Nutraceutical Brands
By Barrier Type
- Moisture Barrier
- Oxygen Barrier
- Light Barrier
Region
- Asia Pacific
- North America
- Latin America
- Europe
- Middle East & Africa